Direct export configurations compliant with NFRC, CE, EN 12020-2, and AS2047 structural and thermal standards for luxury commercial and residential applications.
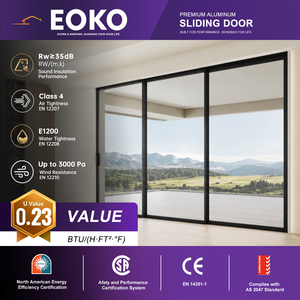
Engineered for luxury villas, featuring multi-chamber polyamide thermal breaks, extreme wind load resistance, and precision heavy-duty rollers.
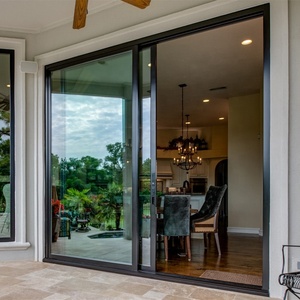
Heavy-gauge UPVC vinyl profiles integrated with German ROTO hardware multi-point locking systems for maximum structural integrity and security.
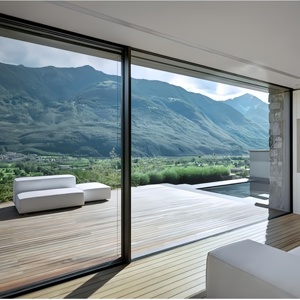
Custom extruded architectural aluminum profile designed for large modern villa balconies, optimized for solar heat gain coefficient control.
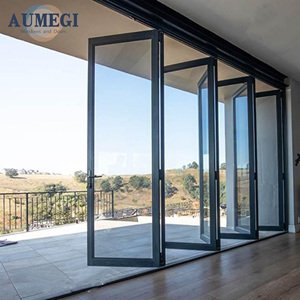
Heavy-duty top-hung bi-folding glass wall system designed to meet AS2047 structural deflection and water ingress prevention criteria.
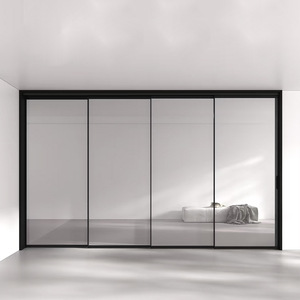
Ultra-narrow interlock sightline (20mm) concealed sliding frame system with recessed track integration for architectural minimalist aesthetics.
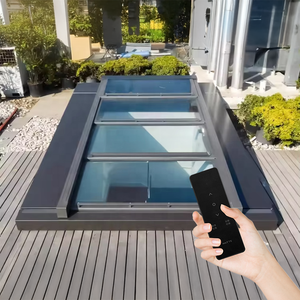
Automated roof access window hatch integrated with IP67 electric actuators, rain sensor inputs, and structural thermal break framing.
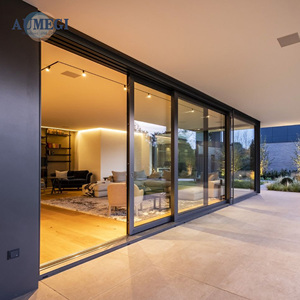
Multi-track extrusion arrangement supporting heavy leaf weights up to 400kg per panel with stainless steel precision guidance tracks.
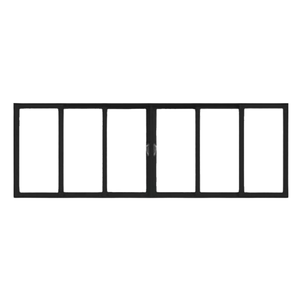
High-rigidity 6063-T6 alloy profile sliding glass wall designed for residential apartments, executive offices, and coastal building envelopes.
The global architectural sector has experienced a profound shift toward high-performance building envelopes. As structural engineers, developers, and commercial procurement heads look to source fenestration systems and window hardware, understanding the manufacturing industrial clusters in China becomes paramount. China’s architectural hardware manufacturing ecosystem produces over 60% of the world’s extruded aluminum profiles, multi-point lock mechanisms, friction stays, and thermal break structural assemblies.
However, navigating supplier capabilities requires looking beyond superficial catalog listings. Premium architectural performance relies on meticulous metallurgy, precise extrusion tolerances adhering to EN 12020-2 standards, and advanced surface treatment chemistry (such as Qualicoat-certified powder coating and Qualanod anodizing). Strategic procurement teams must evaluate factories based on their engineering capacity, quality management systems (ISO 9001:2015), and rigorous laboratory testing regimes covering air permeability (EN 1026), watertightness (EN 1027), and wind resistance (EN 12211).
Utilization of primary 6063-T5 and T6 structural aluminum billets with strictly controlled magnesium and silicon ratios, eliminating internal voids and ensuring uniform tensile strength above 205 MPa.
Integration of high-grade Polyamide PA66-GF25 (25% glass fiber reinforced) structural thermal insulation strips, drastically mitigating thermal bridging and lowering systemic U-values.
Multi-point locks, hinges, and friction stays undergo rigorous lifecycle testing surpassing 50,000 to 100,000 opening/closing cycles under neutral salt spray conditions (ASTM B117).
A detailed comparison matrix of fenestration system engineering metrics used by top-tier OEMs and export manufacturing houses.
| System Category | Structural Profile Alloy | Thermal Transmittance (Uw) | Air Permeability (EN 1026) | Watertightness (EN 1027) | Wind Resistance (EN 12211) |
|---|---|---|---|---|---|
| Triple-Glazed Lift & Slide | 6063-T6 / Wall 2.0mm | 0.85 – 1.1 W/m²K | Class 4 (600 Pa) | Class E1050 (1050 Pa) | Class C5 (2000 Pa) |
| Minimalist Hidden Sliding Door | 6060-T66 / Wall 1.8mm | 1.2 – 1.5 W/m²K | Class 3 (300 Pa) | Class 7A (300 Pa) | Class C3 (1200 Pa) |
| Heavy-Duty Architectural Bi-Fold | 6063-T5 / Wall 2.2mm | 1.3 – 1.7 W/m²K | Class 4 (600 Pa) | Class 9A (600 Pa) | Class C4 (1600 Pa) |
| Unitized Curtain Wall System | 6063-T6 / Wall 3.0mm | 1.0 – 1.4 W/m²K | Class A4 (600 Pa) | Class R7 (750 Pa) | Design Load ≥ 3.0 kPa |
| Motorized Roof Skylight Hatch | 6063-T6 / Wall 2.5mm | 0.9 – 1.2 W/m²K | Class 4 (600 Pa) | Class E1200 (1200 Pa) | Class C5 (2000 Pa) |
In low-energy building design, frame thermal transmittance ($U_f$) is controlled by the depth and geometric configuration of the polyamide barrier. Conventional PVC or non-thermal break aluminum frames suffer from high U-values ($>3.5\text{ W/m}^2\text{K}$), causing severe condensation and HVAC energy loss. Leading Chinese exporters utilize multi-cavity thermal break profiles filled with polyurethane foam inserts, lowering the frame thermal transmittance to pair with Low-E argon-filled triple insulating glass units (IGUs).
How senior project leaders verify manufacturer capabilities, prevent material substitution, and enforce international compliance standards.
Material degradation often occurs when low-tier suppliers mix scrap aluminum into extrusion billets. Professional buyers demand Mill Test Certificates (MTC) traceably linked to specific cast numbers. Spectral analysis must confirm strict adherence to chemical composition limits—specifically controlling Iron (Fe $\le 0.35\%$) to preserve structural ductility and prevent micro-fracturing during crimping.
For coastal and high-humidity installations, powder coating thickness must consistently measure between 60 $\mu\text{m}$ and 80 $\mu\text{m}$. Factories operating automated vertical powder coating lines with pre-treatment chromate-free conversion systems achieve superior adhesion (ISO 2409 Class 0). Salt spray testing must exceed 1,000 hours without blistering or cross-hatch creepage.
Navigating technological evolutions, decarbonization mandates, and smart system integration in global fenestration procurement.
The demand for automated opening elements is accelerating. Modern sliding doors and high-level skylights feature hidden linear actuators, micro-ventilation controllers, and home automation API compatibility, requiring hardware to feature low-voltage wiring pathways inside profiles.
Architectural design continues to prioritize maximum glass area. Emerging hardware configurations move structural hinges completely into frame rebate grooves (concealed 180-degree hinges), supporting leaf weights over 180kg without compromising perimeter gasket sealing.
With carbon border adjustment mechanisms (CBAM) taking effect in Europe, procurement guidelines prioritize extrusions manufactured with hydroelectric power or high recycled content, backed by verified Environmental Product Declarations (EPD).
Operating as a specialized export partner and architectural solutions provider, our manufacturing network bridges complex architectural intent with precision factory production. Unlike trading intermediaries, our engineering desk reviews DWG and BIM models prior to quotation, analyzing wind loads, structural glass dead loads, and hardware torque limits.
Every profile bundle and hardware shipment undergoes rigorous multi-point inspection. We verify extrusion wall tolerances ($\pm 0.05\text{mm}$), corner crimping mechanical strength, and hardware gear engagement smooth operation before sea-freight packing.
Products are packed in ISPM-15 compliant fumigated wooden crates with internal rubber bracing, moisture-absorbing desiccants, and individual elevation coding for efficient site distribution upon arrival.
Technical answers to critical procurement, compliance, and custom hardware engineering inquiries.
Depending on frame depth, polyamide thermal break strip width (ranging from 14.8mm up to 34mm), and double or triple Low-E argon glass build-ups, our systems achieve systemic Uw values from 1.8 W/m²K down to ultra-insulated passive house levels of 0.85 W/m²K. Exact U-values are calculated per project project elevation dimensions.
For seaside or high-salinity environments, we supply hardware manufactured from SS316 stainless steel or aluminum components treated with multi-layer electroplated finishes. These systems are tested under ISO 9227 neutral salt spray conditions for over 1,000 hours without structural base metal oxidation.
Every commercial export order includes a full technical dossier containing shop drawings, extrusion profile cross-section CAD files, Mill Test Certificates (MTC) for alloy chemical composition, hardware cycle test reports, and CE/NFRC compliance statements.
Yes. Our engineering division provides custom OEM/ODM hardware design services. We manufacture custom transmission gear rods, specialized corner drives, and heavy-duty roller carriages tailored to proprietary extrusion euro-groove dimensions.
We work flexibly on a project container consolidation basis rather than enforcing strict piece counts. A standard consolidated 20ft or 40ft container containing windows, doors, and matching hardware takes approximately 25 to 35 days from shop drawing approval to factory dispatch.
Submit your architectural DWG elevations or window schedules. Our senior engineering team will return profile recommendations, thermal calculations, and factory-direct pricing within 48 hours.
